Global sourcing for precision cnc machining is no longer just a search for low quotes. Buyers need stable tolerances, traceable inspection records, and dependable delivery across repeated production runs. Grand View Research valued the global CNC machine market at $101.22 billion in 2023 and forecast 7.3% annual growth from 2024 to 2030. That figure covers CNC machines broadly, not precision machining services alone. The distinction matters when comparing suppliers.
The 2025 International Federation of Robotics report recorded 542,000 industrial robots installed worldwide in 2024, more than double the total a decade earlier. Automation is changing factory capacity, but it does not guarantee a good part. A supplier still needs skilled programmers, calibrated equipment, and inspection methods suited to the drawing. A neat website cannot prove any of that.
Shigeo Shingo, a leading Japanese manufacturing engineer and quality expert, warned, “The most dangerous kind of waste is the waste we do not recognize.” His point applies to sourcing: hidden setup delays or weak process control can cost more than a higher unit price. Yet no ranking can fully capture a supplier’s day-to-day discipline. This guide compares companies using practical signals, including machining capabilities, quality systems, industry experience, and support for international buyers. Treat the shortlist as a starting point, not a verdict. Ask for evidence. Check the details. A small omission can become an expensive surprise.
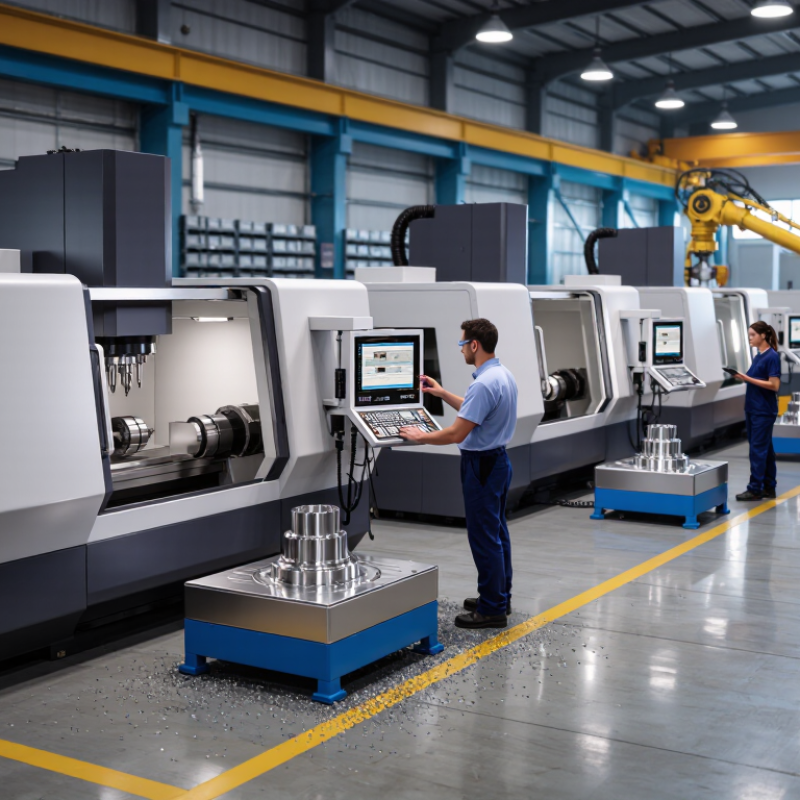
For global buyers, axis count affects more than speed. It shapes setup time, tool access, accuracy, and the number of operations required. A 3-axis machine moves along X, Y, and Z, making it suitable for flat plates, pockets, and straightforward housings. Each repositioning can introduce alignment error. A 4-axis machine adds rotary motion, allowing features around a part’s circumference to be cut with fewer setups. That can help with shafts and indexed holes. A 5-axis machine tilts or rotates the tool or workpiece, reaching angled surfaces and complex contours. It is capable, but not automatically better.
The investment is substantial. Grand View Research estimated the global CNC machine market at USD 101.22 billion in 2023 and projected 5.3% annual growth from 2024 to 2030. This figure covers the broader CNC machine market, not precision machining alone. It signals expanding adoption, but says little about whether a particular part needs five axes. A thin aluminum bracket may run efficiently on three; a contoured turbine component may justify five.
Look beyond the machine count. Ask about workholding, tool reach, inspection routines, and demonstrated tolerances. For example, a shop can show how it measures a deep bore after machining, not just quote a tolerance. More axes can reduce handling, yet programming and verification become harder. That sounds simple. It isn’t. Even experienced buyers can over-specify a process before reviewing the drawing, material, and annual volume.
For global buyers, ±0.025 mm (±0.001 in) is a useful CNC machining benchmark, not a guaranteed result on every feature. A short, accessible hole may hold this tolerance more readily than a deep bore or thin wall that flexes during cutting. Material also matters: aluminum, stainless steel, and plastic respond differently to heat and tool pressure. Small shifts count. A part can measure correctly while warm, then drift slightly as it reaches room temperature.
Clear drawings make this target more meaningful. Identify the critical dimensions, datum surfaces, and mating parts, rather than applying a tight tolerance to every edge. For a precision bore, specify how it should be measured; a bore gauge or coordinate measuring machine may reveal issues that a simple caliper misses. Inspection conditions matter too, including instrument calibration and temperature. It is tempting to treat ±0.025 mm as a shop-wide promise. That assumption deserves a second look. Ask suppliers which features they routinely inspect, how they handle out-of-tolerance results, and whether their quoted capability applies to the full production run. A tiny dimension can carry a large consequence.
For global buyers, supplier certificates are useful starting points, not proof of perfect machining. ISO 9001 indicates a documented quality management system and controlled processes. Ask for the current certificate, its scope, and the address of the production site. A certificate held by a company office may not cover the workshop making your parts.
AS9100 adds aerospace-focused controls, including stronger attention to risk, configuration, and traceability. IATF 16949 is tailored to automotive supply chains, where process consistency and corrective action matter. Choose credentials that fit the part’s end use. Details matter. Check whether the supplier’s certified scope includes CNC machining, inspection, and any outsourced operations relevant to your order.
Then look beyond the paperwork. Request sample inspection reports, calibration records, and a clear explanation of how nonconforming parts are contained. For a machined aluminum housing, that may mean reviewing bore measurements, datum references, and material records together. A clean PDF is not a finished part. A trial run can reveal more, though it may not predict every production issue. Certificates build confidence; measured results and honest communication help keep it.
Supplier credentials: ISO 9001, AS9100, and IATF 16949
This chart compares the publication years of the standards’ referenced editions, not the number of certified suppliers. ISO 9001:2015 was published in 2015; AS9100 Rev D and IATF 16949:2016 were published in 2016. Buyers should verify each supplier’s current certificate, scope, and issuing body.
Comparing precision CNC machining companies starts with the work they can actually produce. A machine list is useful, but it does not show whether a shop can hold a tight tolerance across a complex part. Ask for sample inspection reports, typical tolerance ranges, and details on in-process checks. A polished capability sheet can still leave gaps.
Material experience matters. Aluminum parts may need clean edges and stable dimensions after milling, while stainless steel can require careful control of heat and tool wear. Ask how the supplier manages your specific alloy, surface finish, and part geometry. That matters. A quote based on the wrong material grade can distort both cost and delivery estimates.
Compare lead times by stage: engineering review, first article, production, and shipping. Request a schedule tied to your quantity and drawing revision, not just a general promise. Global reach also involves communication across time zones, export documentation, and reliable packaging for parts with delicate features. Confirm who handles each handoff. A low freight estimate is not the whole picture. In practice, even a strong supplier may miss an early estimate when tooling or inspection needs change; that possibility deserves a clear discussion before the order is placed.
A capable precision CNC partner should make design-for-manufacturing (DFM) review a working conversation, not a box-ticking form. Before quoting, ask the engineering team to flag thin walls, deep pockets, tight internal corners, and tolerances that drive cost without improving function. A 0.2 mm wall may look fine on screen, yet chatter or distortion can appear after machining. Request annotated drawings or a marked-up 3D model, with proposed changes clearly separated from your original requirements. DFM comments should address stock, tool access, datum choices, and finishing allowances, not just say “machinable.” Small details matter.
For a first-article inspection (FAI), agree on the sample quantity, revision level, and acceptance criteria before production starts. The report should link each drawing characteristic to an actual measurement, instrument, and result. Ask for critical dimensions to be checked on the first physical parts, including hole positions, flatness, and threaded features. Keep the sample traceable to its material lot and process route. Photos can help, but they cannot replace recorded measurements. One awkward point: supplier formats vary, so a polished report may still omit a dimension you care about.
CMM reports are useful for complex profiles and positional tolerances, but only when the inspection setup is understood. Confirm the datum alignment, probe strategy, units, and calibration status; request a readable report alongside the drawing balloon map. For international projects, settle file naming, units, and approval timing across time zones. Ask who reviews nonconformances and how revisions are controlled. A quick video call over a flagged feature can prevent weeks of email, though it is not a substitute for documented approval. Examine a sample report before selecting a supplier.
| Evaluation Area | What to Request | Evidence to Review | Buyer Acceptance Check |
|---|---|---|---|
| Design for Manufacturability (DFM) | A documented review of the 2D drawing and 3D model before production, including questions about tolerances, tool access, thin walls, deep features, datums, and inspection requirements. | Marked-up drawing or model, written risk list, and proposed changes clearly identified for buyer approval. | Confirm that no drawing or model change is made without written approval. Check that the supplier has identified features that may affect cost, lead time, or inspectability. |
| Drawing and Tolerance Control | Confirmation of the drawing revision, units, material condition, surface finish, geometric tolerances, and any general tolerance standard specified by the buyer. | Revision-controlled quotation, production drawing, and inspection plan referencing the same document revision. | Do not assume a general tolerance applies when the drawing is silent. Agree on the applicable tolerance standard and class in the purchase documents. |
| Material Verification | Material grade, condition, and required traceability level, as defined by the drawing or purchase order. | Material test certificate or supplier certificate showing the specification, grade, heat or lot identification, and linkage to the supplied parts when required. | Check that the certificate matches the ordered material specification and that lot or heat numbers can be traced to the parts where traceability is required. |
| First-Article Inspection (FAI) | A first-article inspection against all drawing characteristics before release of the production batch. For regulated or customer-controlled work, confirm the required FAI format in advance. | Ballooned drawing and characteristic-by-characteristic results, with actual measurements, units, inspection method, and disposition of any nonconformity. | Verify that every required characteristic is accounted for and that the report identifies the part number, revision, sample, and inspection date. AS9102-based reporting is applicable when required by the customer or contract; it is not a universal requirement for all machined parts. |
| CMM Reports | Coordinate Measuring Machine results for specified dimensions and geometric characteristics, using agreed datums, alignment, and measurement strategy. | Report identifying the part and revision, measured features, nominal values, tolerances, actual results, units, and pass/fail status. | Check that the report covers the characteristics requested by the drawing or inspection plan. A CMM report does not replace other methods when a feature requires a different inspection technique. |
| Measurement Equipment | Information on the equipment and measurement methods used for acceptance inspection, including calibration status. | Equipment identification and current calibration records or traceability information appropriate to the measurement task. | Confirm that the measurement method is suitable for the tolerance and feature being checked. ISO/IEC 17025 accreditation is relevant when an accredited laboratory is contractually required; it is not automatically required for every machine shop. |
| Quality Management | Details of the quality controls used for incoming material, in-process checks, final inspection, nonconforming product, and corrective action. | Quality-system certificate, inspection procedures, sample records, and nonconformance or corrective-action process details, as applicable. | Where ISO 9001 certification is required, verify the certificate scope, validity, and issuing certification body. Certification alone does not establish that a specific part meets its drawing requirements. |
| Surface Finish and Secondary Operations | Confirmation of specified surface roughness, deburring, edge condition, coating, heat treatment, or other post-machining requirements. | Inspection results or process certificates for the requirements that apply to the part and purchase order. | Check the drawing for the measurement parameter, units, sampling location, and any post-treatment condition. Agree how cosmetic and functional surfaces will be evaluated. |
| Production Consistency | A defined sampling and in-process inspection plan for repeat orders, including controls for critical or customer-designated characteristics. | Control plan, inspection records, process-change notification procedure, and batch or lot identification where required. | Agree on sampling frequency and escalation rules before production. Require approval for changes that could affect form, fit, function, material, or inspection results. |
| Packaging and Delivery | Packaging method, preservation requirements, labeling, shipping documents, and delivery terms appropriate to the part and destination. | Packaging specification, sample label, packing list, and agreed shipment documentation. | Confirm protection against corrosion, impact, contamination, and part-to-part contact where relevant. Match quantities, part numbers, revisions, and lot identifiers to the order. |
Buyer note: Define acceptance criteria, applicable standards, required report formats, sampling levels, and document language in the drawing, quality agreement, or purchase order. Requirements vary by part, industry, and contract.